Tap drill size chart and calculator for every thread
Every tapped hole starts as a drilled one, and the drill has to be right. If it’s too small the tap jams, and small taps snap off in the hole. A drill that’s a bit big leaves a shallow thread that strips easily. Here are the drill sizes for metric, UNC and UNF threads, and below them a calculator that shows the hole being drilled and tapped.
For fine threads such as M10 × 1.25, use our tap drill calculator, which has them too.
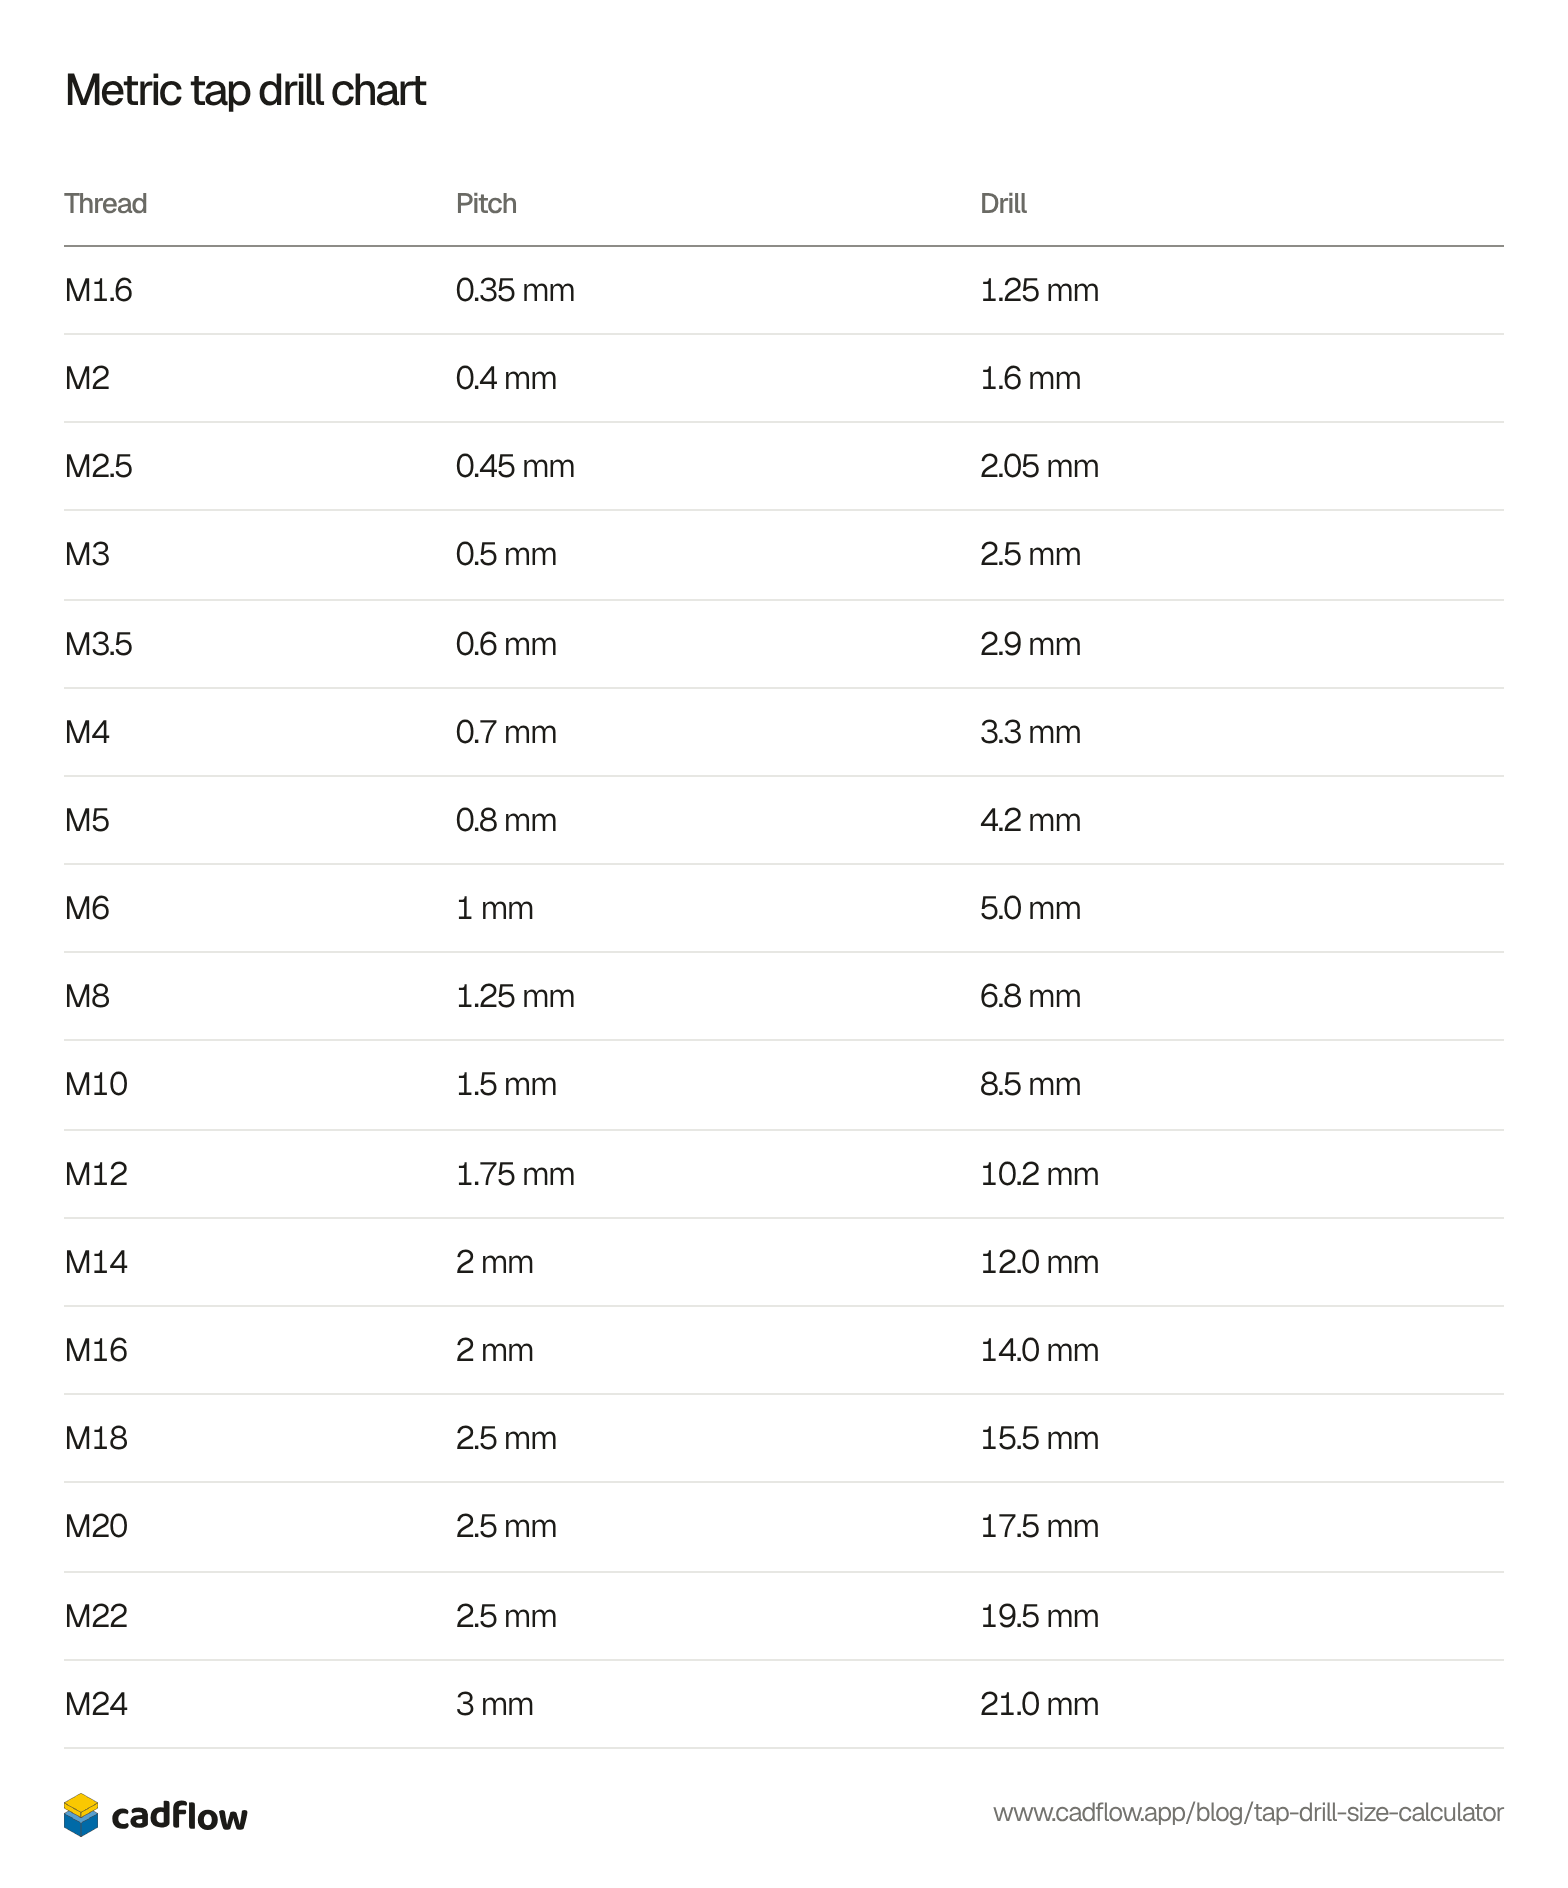
| Thread | Pitch | Drill |
|---|---|---|
| M1.6 | 0.35 mm | 1.25 mm |
| M2 | 0.4 mm | 1.6 mm |
| M2.5 | 0.45 mm | 2.05 mm |
| M3 | 0.5 mm | 2.5 mm |
| M3.5 | 0.6 mm | 2.9 mm |
| M4 | 0.7 mm | 3.3 mm |
| M5 | 0.8 mm | 4.2 mm |
| M6 | 1 mm | 5.0 mm |
| M8 | 1.25 mm | 6.8 mm |
| M10 | 1.5 mm | 8.5 mm |
| M12 | 1.75 mm | 10.2 mm |
| M14 | 2 mm | 12.0 mm |
| M16 | 2 mm | 14.0 mm |
| M18 | 2.5 mm | 15.5 mm |
| M20 | 2.5 mm | 17.5 mm |
| M22 | 2.5 mm | 19.5 mm |
| M24 | 3 mm | 21.0 mm |
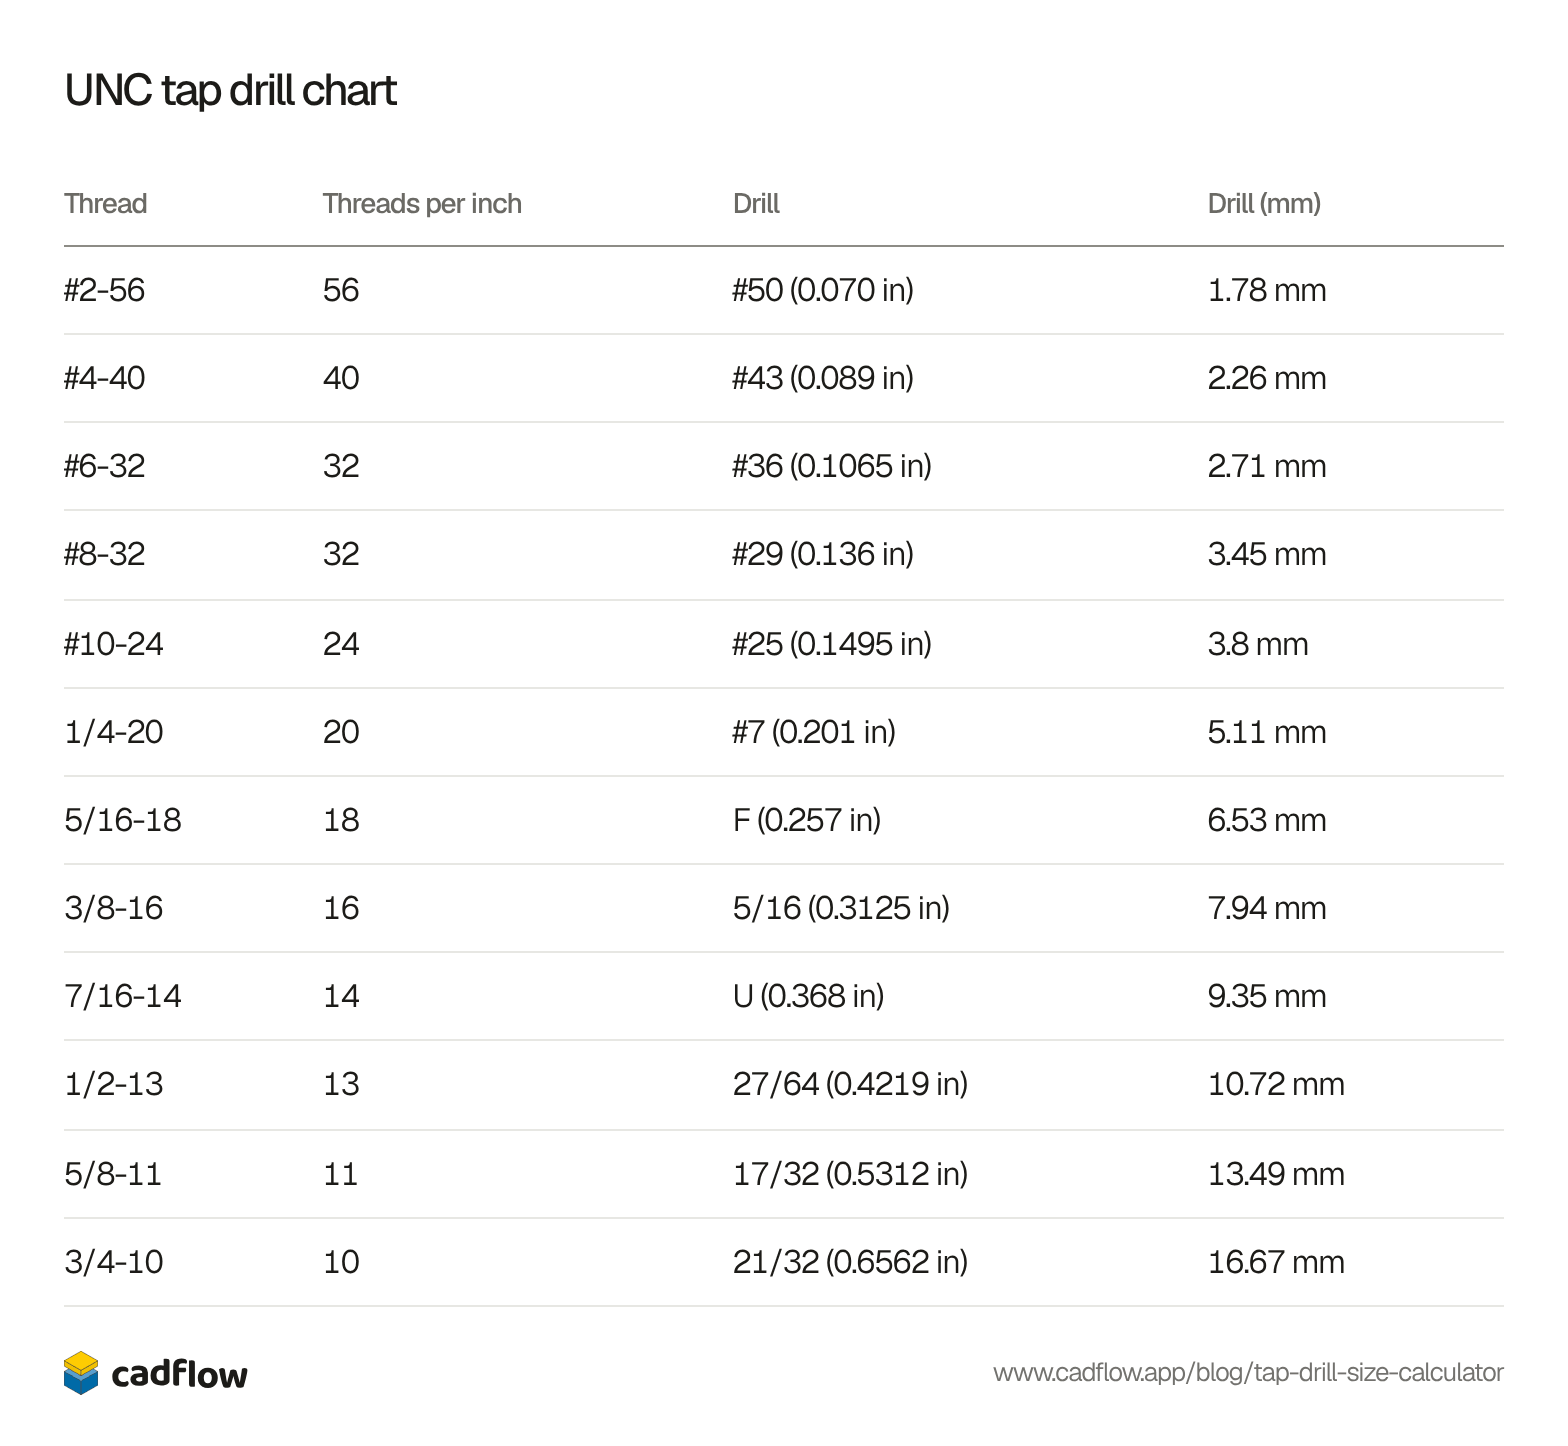
| Thread | Threads per inch | Drill | Drill (mm) |
|---|---|---|---|
| #2-56 | 56 | #50 (0.070 in) | 1.78 mm |
| #4-40 | 40 | #43 (0.089 in) | 2.26 mm |
| #6-32 | 32 | #36 (0.1065 in) | 2.71 mm |
| #8-32 | 32 | #29 (0.136 in) | 3.45 mm |
| #10-24 | 24 | #25 (0.1495 in) | 3.8 mm |
| 1/4-20 | 20 | #7 (0.201 in) | 5.11 mm |
| 5/16-18 | 18 | F (0.257 in) | 6.53 mm |
| 3/8-16 | 16 | 5/16 (0.3125 in) | 7.94 mm |
| 7/16-14 | 14 | U (0.368 in) | 9.35 mm |
| 1/2-13 | 13 | 27/64 (0.4219 in) | 10.72 mm |
| 5/8-11 | 11 | 17/32 (0.5312 in) | 13.49 mm |
| 3/4-10 | 10 | 21/32 (0.6562 in) | 16.67 mm |
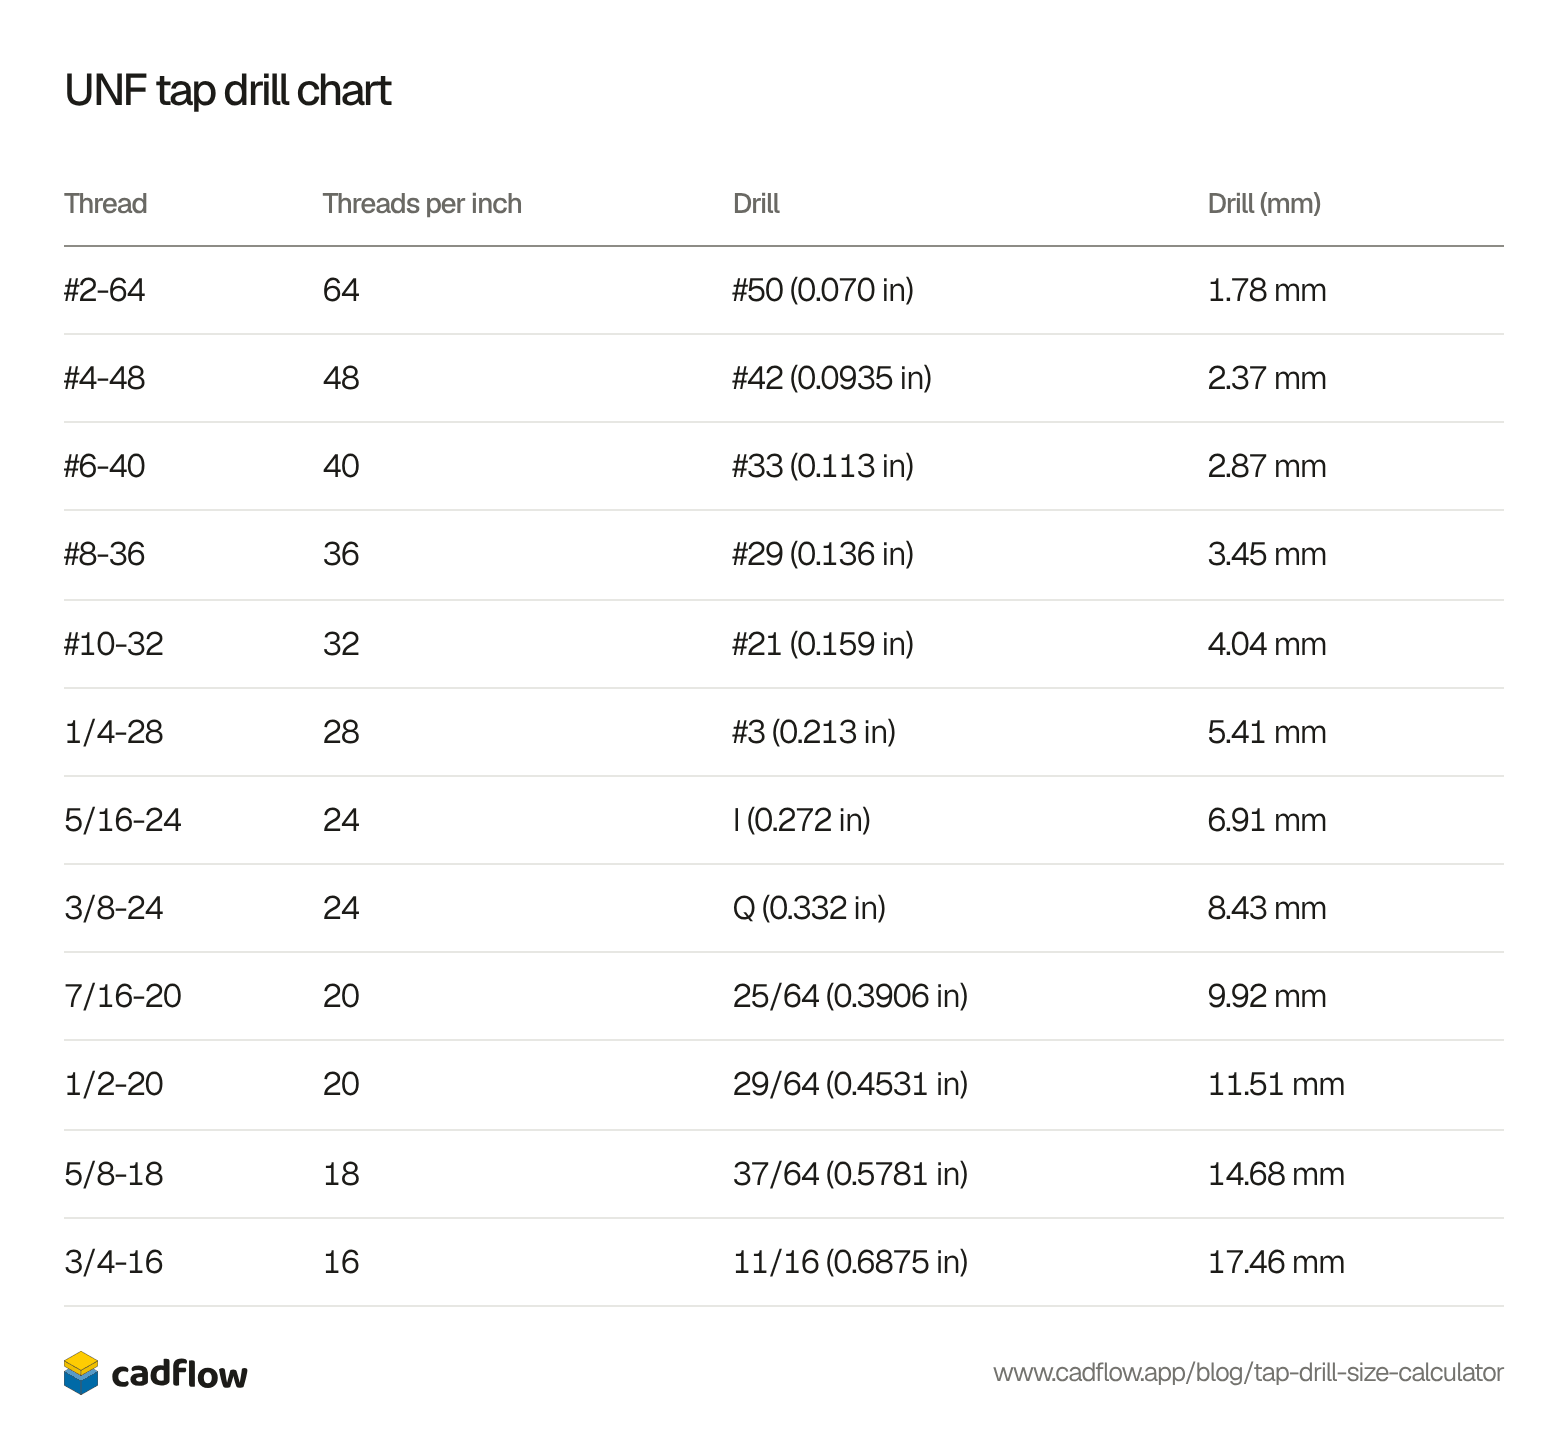
| Thread | Threads per inch | Drill | Drill (mm) |
|---|---|---|---|
| #2-64 | 64 | #50 (0.070 in) | 1.78 mm |
| #4-48 | 48 | #42 (0.0935 in) | 2.37 mm |
| #6-40 | 40 | #33 (0.113 in) | 2.87 mm |
| #8-36 | 36 | #29 (0.136 in) | 3.45 mm |
| #10-32 | 32 | #21 (0.159 in) | 4.04 mm |
| 1/4-28 | 28 | #3 (0.213 in) | 5.41 mm |
| 5/16-24 | 24 | I (0.272 in) | 6.91 mm |
| 3/8-24 | 24 | Q (0.332 in) | 8.43 mm |
| 7/16-20 | 20 | 25/64 (0.3906 in) | 9.92 mm |
| 1/2-20 | 20 | 29/64 (0.4531 in) | 11.51 mm |
| 5/8-18 | 18 | 37/64 (0.5781 in) | 14.68 mm |
| 3/4-16 | 16 | 11/16 (0.6875 in) | 17.46 mm |
5.0 mm
drill for an M6 tap
Thread 6.0 mm across, 1 mm pitch
Why M6 takes a 5 mm drill
For metric threads you take the pitch off the size. M6 has a 1 mm pitch, so 6 minus 1 gives 5 mm. M8 has a 1.25 mm pitch, which gives 6.75, and the chart rounds that to the 6.8 mm drill you can actually buy.
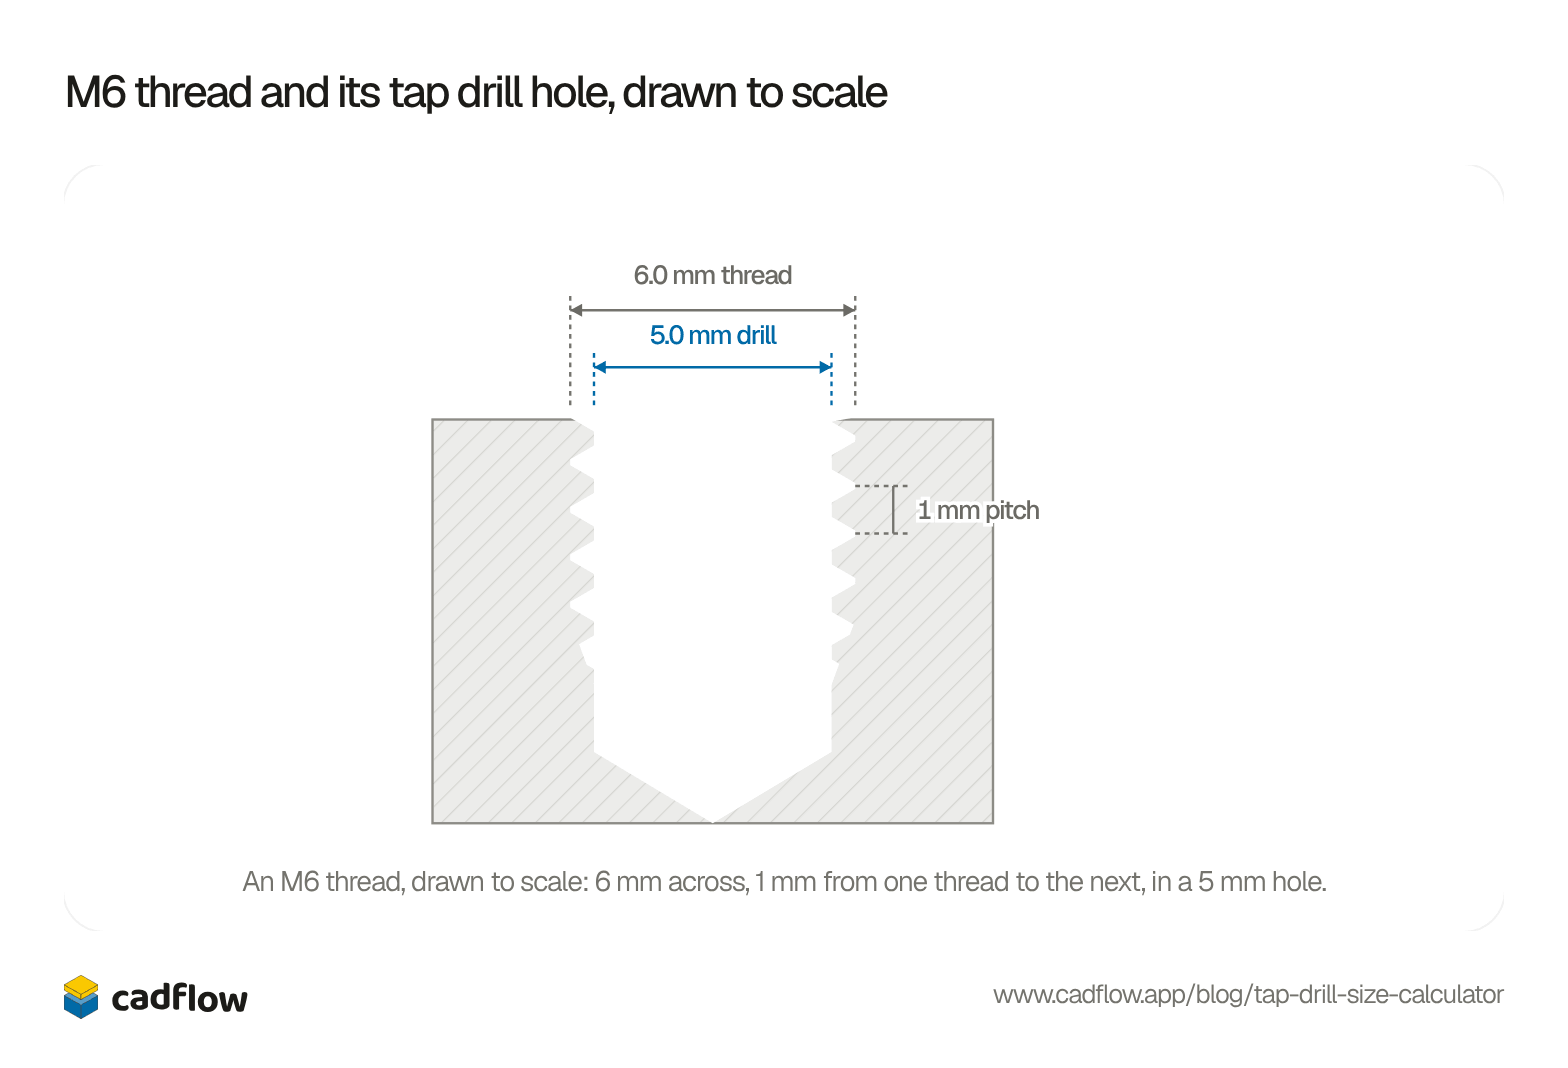
That leaves about 75% of a full thread, which is what tap drill charts aim for, as the tap and die article on Wikipedia explains. Inch drills come in numbered and lettered sizes like #7 and F, so for those you read the chart. Our metric sizes are ISO 2306’s, as tabled by AmesWeb, and the inch ones are the 75% column of Little Machine Shop’s chart.
Going a size up in hard metals
Steel, stainless and cast iron are hard work for a hand tap, and a slightly bigger drill helps alot. Little Machine Shop’s chart gives 5.4 mm for M6 instead of 5.0, 7.2 mm for M8 instead of 6.8 and 9.0 mm for M10 instead of 8.5. That leaves a 50% thread, with less metal for the tap to cut.
Tapping the hole
Drill straight, because the tap follows the hole. Take the sharp edge off the top with a countersink so the tap starts square, and use cutting oil in steel (cast iron is tapped dry, according to Wikipedia). Then turn the tap in, backing it off a little every so often to break the chip, since chips packing into the flutes are what snap taps.
- 1Drill it straight
- 2Take the edge off
- 3A drop of oil
- 4Tap in, back off, repeat
In a blind hole, drill deeper than the thread you need. A plug tap tapers over its first 3 to 5 threads and can’t cut a full thread right at the bottom, which you can see at the bottom of the hole above.
Tapping 3D prints
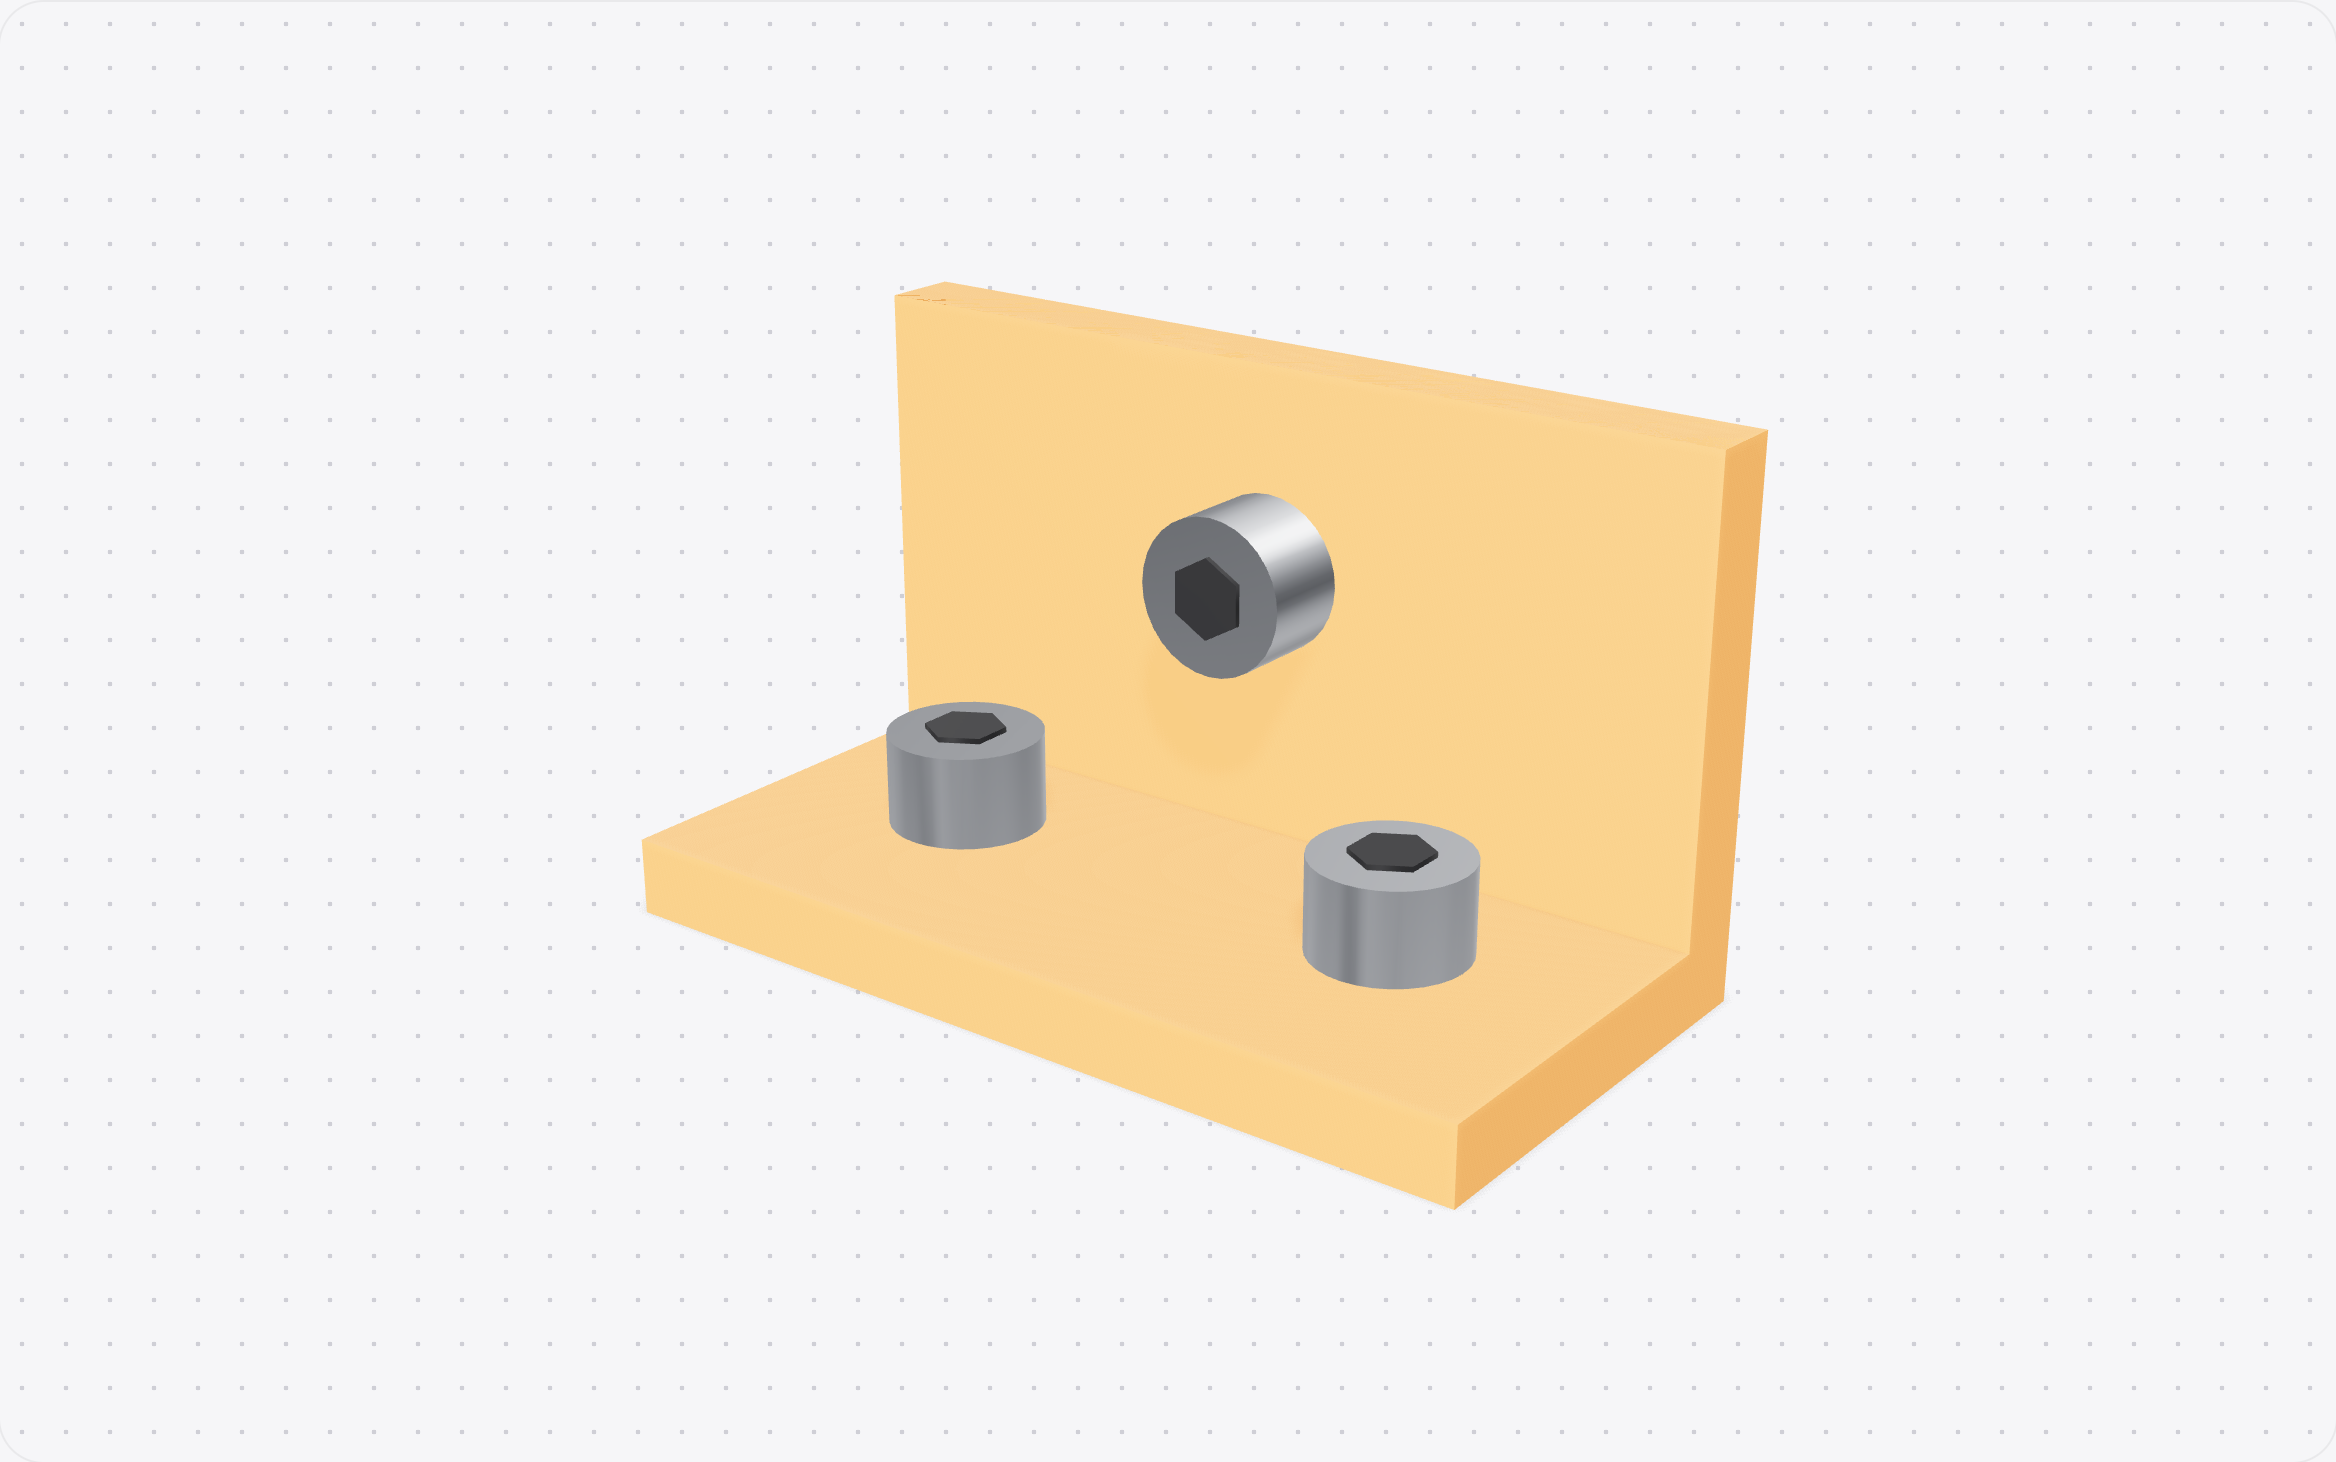
Printed holes tap fine. Draw them at the drill size from the chart, and print a small test piece and adjust untill the fit is right, because printed holes tend to come out a little smaller than drawn. Our L-bracket has three 5 mm holes for exactly this, and you can download it from the library.
We make CadFlow, CAD in the browser for parts you’re going to print, cut or saw. It isn’t public yet.
Questions people ask
What size drill for an M3 tap?
2.5 mm.
What size drill for an M6 tap?
5.0 mm, or 5.4 mm in steel or stainless.
What size drill for a 1/4-20 tap?
A #7 drill, which is 0.201 in or 5.11 mm.
Is the drill the same size as the screw?
No, it's smaller, because the tap cuts the thread into the wall of the hole. A hole the size of the screw is a clearance hole, and the screw slides through it without gripping.
Free tools for this
History of this post
- Updated: The drill sizes people ask for most at the top.
- Published
Read next
Metric bolt size chart: spanner and hex key sizes, M2 to M24
Tensile and yield strength: steel, aluminium, bolts, wood and plastic
Raised garden bed plans: a 4 × 8 ft bed from nine 2x6s


This blog is by the team making CadFlow, where you build your project in 3D and show how it goes together.
See how CadFlow works